
RedSight®
Design-guided intelligent inspection for high-mix, low-volume manufacturing
RedSight® inspects each unit against its own design data, not a learned baseline.
For control cabinets, harness boards, fixtures, racks and pallets.
Patent pending. Runs on-site, with no cloud dependency.
Every unit is different. Every unit needs checking.
If you build in small batches or to order, no two units are quite alike. This is high-mix manufacturing: many variants, low volumes, and every build differs from the last.
That breaks the usual intelligent inspection approaches. A reference image can’t distinguish an acceptable difference from a real fault, and there aren’t enough samples to train a vision model. In a dense assembly, parts also hide behind other parts, so a fixed camera cannot see everything it needs to.
So the check falls back to people. Manual inspection is slow, varies between shifts, and it’s easy to miss a missing, misplaced, or wrong part.
Inspection that starts from the design files you already have
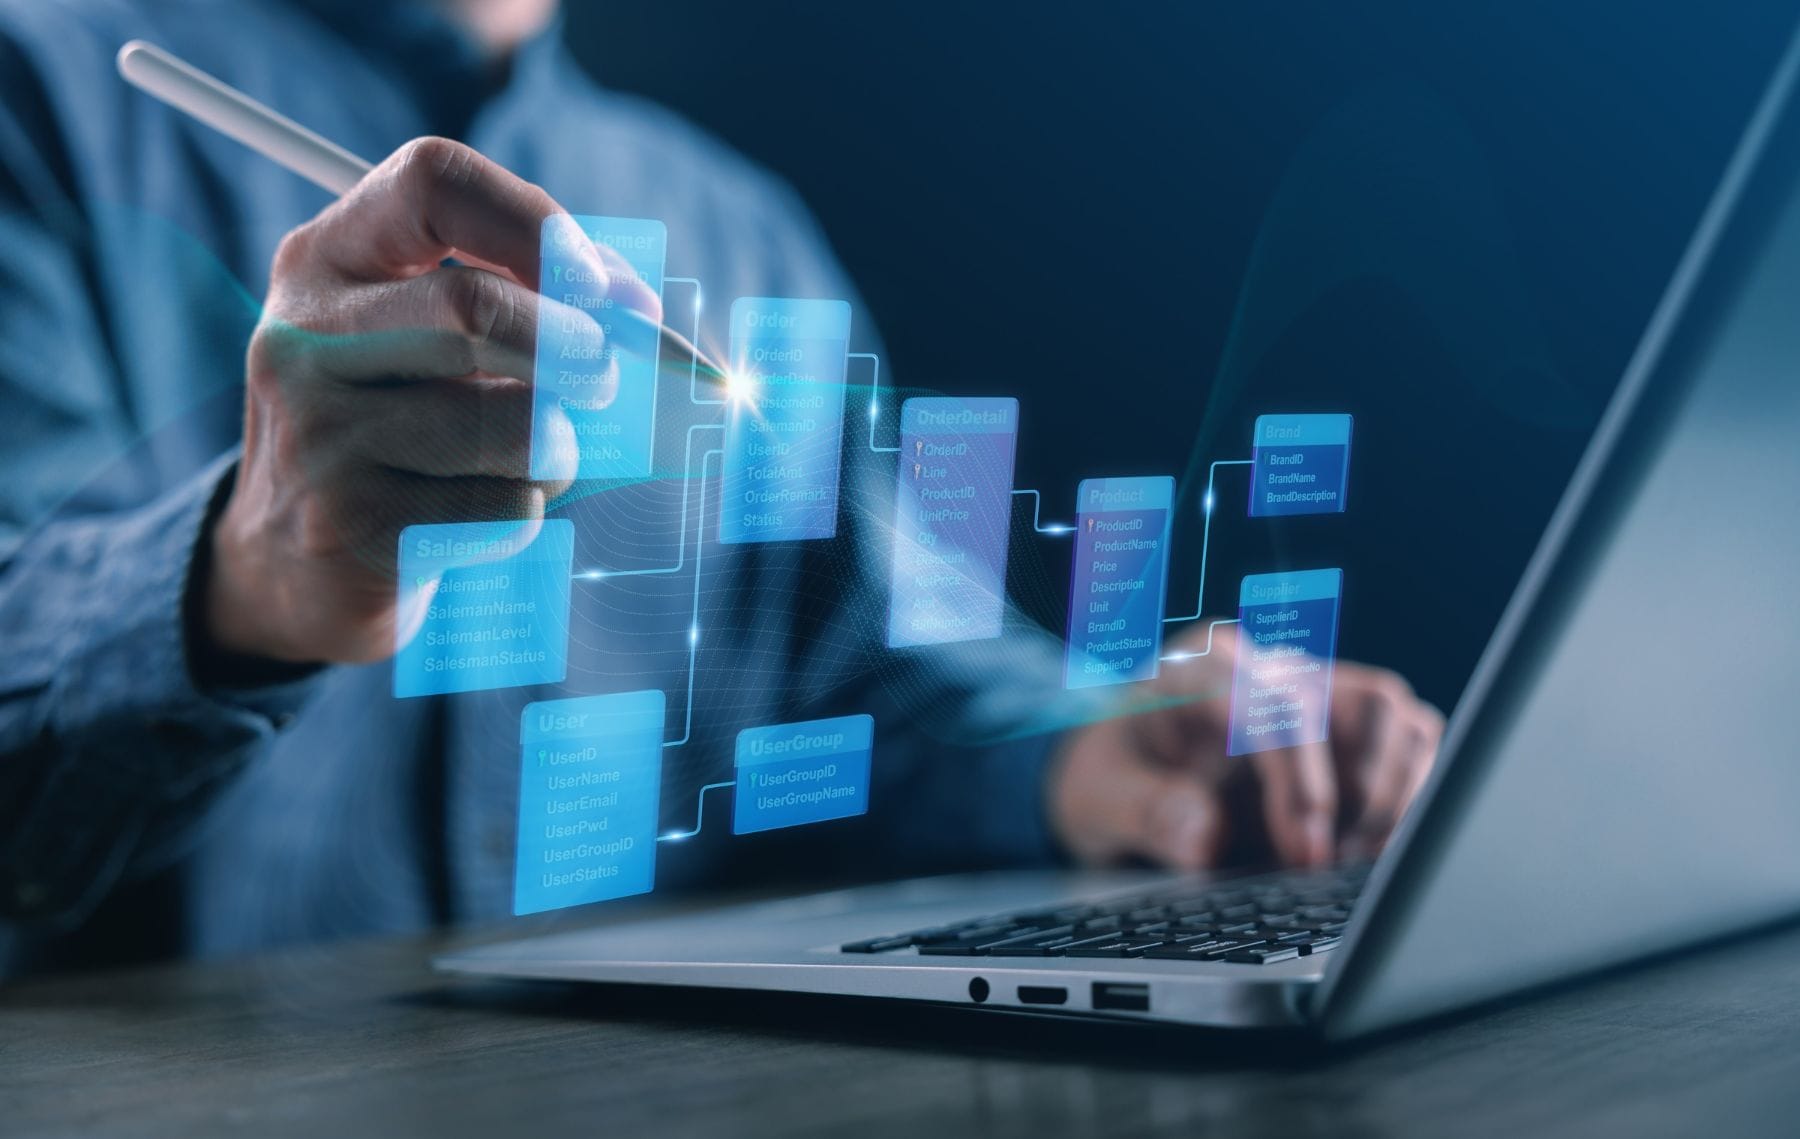
RedSight reads the design data you already hold for your product. It compares what the cameras see with that design, so the system knows what should be there before it inspects anything. You do not need to build a reference unit or a library of sample images.
A conventional vision model flags whatever looks different from what it has learned. RedSight asks a different question: does this unit match its design? Variation between builds is expected, so it is not treated as noise.
See RedSight in action
RedSight Wire inspecting a control cabinet against its design
A cobot moves the camera around a control cabinet. RedSight checks each part and wire against the cabinet’s design data, shows any fault on the physical cabinet, and stores the result with the unit. RedSight Wire is one application of RedSight.
How RedSight works
RedSight turns your design data into a repeatable inspection in four steps.
Load the design
Import the product design files you already have.
Capture and train
Cameras capture product images from exact, repeatable positions. RedSight builds a model of the product piece by piece, matches what it sees to the design, and automatically labels the training images. Nobody labels images by hand.
Inspect every unit
Image each unit from the same positions and check it against its design from multiple angles, as needed.
Report and record
You get a pass-or-fail result with the fault pinpointed and explained, and a record stored for traceability.
Benefits of RedSight
Consistent, dependable inspection
Every unit is checked the same way against its design, across shifts, lines and sites.
Built for high-mix variation
Each unit is checked against its own design, so differences between builds are expected.
No cloud dependency
Inspection runs on site with no cloud round trip, and your data stays under your control.
Faster training and set-up
Validating against design data trains faster than a traditional visual-comparison model, cutting set-up time.
Automated training
RedSight automatically labels training images, so no operator has to label them by hand.
Deploy it the way your line works
RedSight is designed to integrate with your existing line, including sites with legacy equipment, so you can improve inspection without redesigning production or slowing it down. The inspection architecture, models and deployment pipeline are the same, regardless of how you mount the camera, and you stay free to choose or switch your camera, robot and computing hardware vendors. Pick the option that fits your line:
Fixed-mounted
Where access is straightforward, RedSight runs on a fixed camera or a flat X-Y rig at an inspection station.
Cobot-mounted
Where access is constrained or features are hidden behind others, a camera on a collaborative robot moves around the product, inspects from multiple angles and reaches areas a static camera cannot.
Your existing cameras
RedSight can also run on your existing cameras, including CCTV, so you don’t have to add new ones.
Engagement: Start with your inspection problem; prove it on your product
We work in stages, so you see results before committing to a wider roll-out:
Feasibility study
A study on your parts and samples, led by your inspection challenge rather than the solution, so you can see what RedSight will find in your product before committing to a build.
We check your design data and sample parts as part of this study.
Demonstrator
Where it helps, we show fixed and cobot-enabled inspection side by side for your use case.
Pilot
We prove it on a single inspection task.
Roll out
You scale in phases, integrated with your existing production and quality systems. Optional support covers ongoing model refinement.
RedSight Wire: a practical use case
RedSight Wire is an application of RedSight for wiring and cabinet assembly, using a camera-equipped cobot. Control cabinets are dense, vary from build to build, and hide connections behind other components, making multi-angle inspection against the design necessary.
Here, the design data includes the cabinet’s components and wiring.
The cobot moves the camera around the cabinet, captures images from exact, repeatable positions and recreates the same views on each unit.
RedSight finds each part and wire and checks them against the design across multiple images. It identifies any faults in the assembly and reports these clearly for remediation.
Talk to us about your high-mix inspection challenge
We’ll review your inspection challenges, data availability and production constraints, then outline a practical intelligent inspection approach with clear costs, risks and timelines.
Frequently Asked Questions
-
What is RedSight®?
RedSight is Consult Red’s patent-pending design-guided inspection solution for high-mix manufacturing. It imports a product’s design data and checks every unit against that specification, so it knows what should be there, not just whether something looks different.
RedSight Wire is its application to wiring and cabinet assembly, using a camera on a collaborative robot.
-
How is RedSight different from conventional machine vision?
Conventional vision inspection typically compares images with a reference unit, or flags anything that differs from what a model has learned is normal. RedSight compares what the camera sees with the product’s design specification, so it can distinguish a missing or incorrect part from an acceptable difference between units.
-
Do we need a large set of sample images?
RedSight validates against your design data instead of learning from a large set of sample images, so it trains faster than a traditional visual-comparison model. That matters for low-volume, made-to-order products, where samples are scarce. We start with a feasibility study on your parts and samples to confirm what it will find in your product.
-
Does RedSight need the cloud?
No. RedSight can run on-site with no cloud dependency, so inspections don’t wait for a cloud round trip. Web-based tooling for model training is optional, not required.
-
Do we need to buy a robot or new cameras?
No. A cobot is one way of mounting the camera, used where access is constrained or features are hidden. Where access is straightforward, RedSight can run on a fixed camera or flat X-Y rig, or on cameras you already have, including CCTV. You choose your camera, robot, and computing hardware vendors because RedSight isn’t tied to one supplier.
-
Who is RedSight for?
RedSight is built for high-mix manufacturing: high-value, low-volume products where every build differs, and manual checks are slow. Typical users include control panel builders, industrial OEMs with complex inspection needs, and manufacturers in regulated or high-security sectors such as aerospace, defence, and infrastructure.
RedSight starts from product design specifications, so if you have an assembly with design data and an inspection challenge, talk to us.
Related Insights
Articles
Generative AI at the Edge: What’s Possible in 2026
Advances in NPU capabilities and quantization have enabled more sophisticated AI models running locally for low-latency, lower-cost and secure applications.
Case Studies
Long distance HD video over copper for minicam
minicam needed to upgrade its camera systems from SD to HD without replacing existing copper cabling.
Articles
NPUs vs CPUs for Edge AI Vision: Less Heat, Less Power, More Headroom
Benchmarking industrial PPE detection – Raspberry Pi 5 vs Qualcomm QCS6490 (Rubik Pi 3)